What we do
Built for the parts other shops decline.
Our machining discipline was developed on components that operate thousands of feet underground, where a sealing surface, thread, or bore that is almost right is a failure. That standard now serves buyers in aerospace, defense, energy, and industrial markets who need a manufacturer that can take a difficult print and own it end to end.
01 Turning
Multi-axis turning and mill-turn
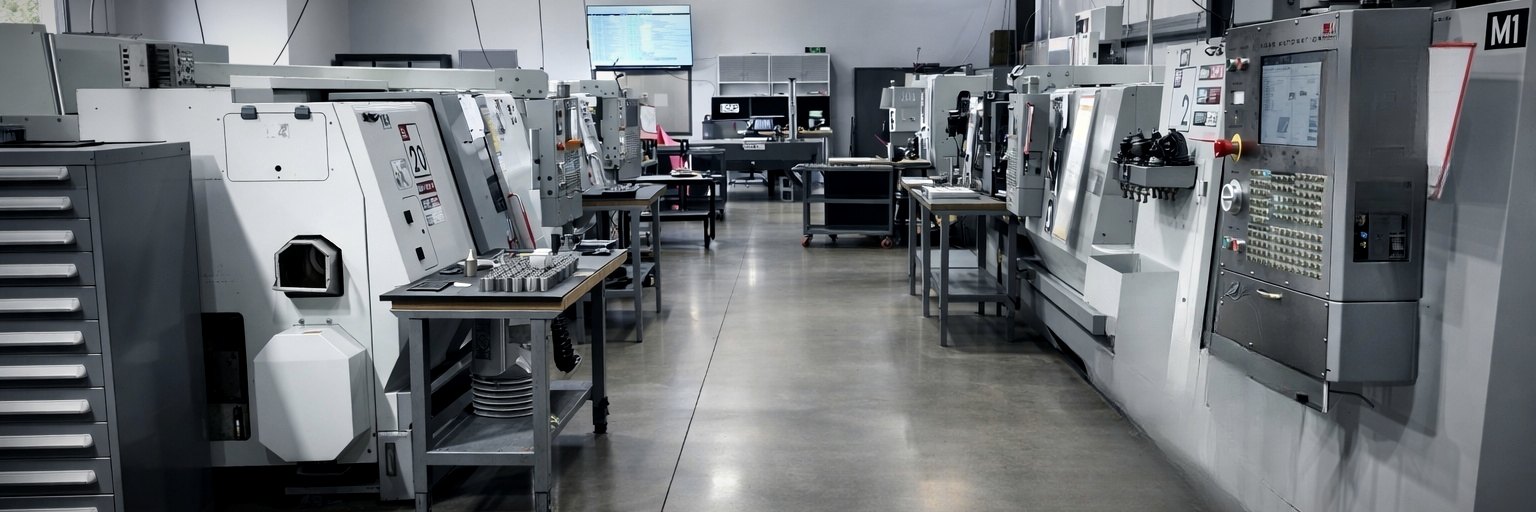
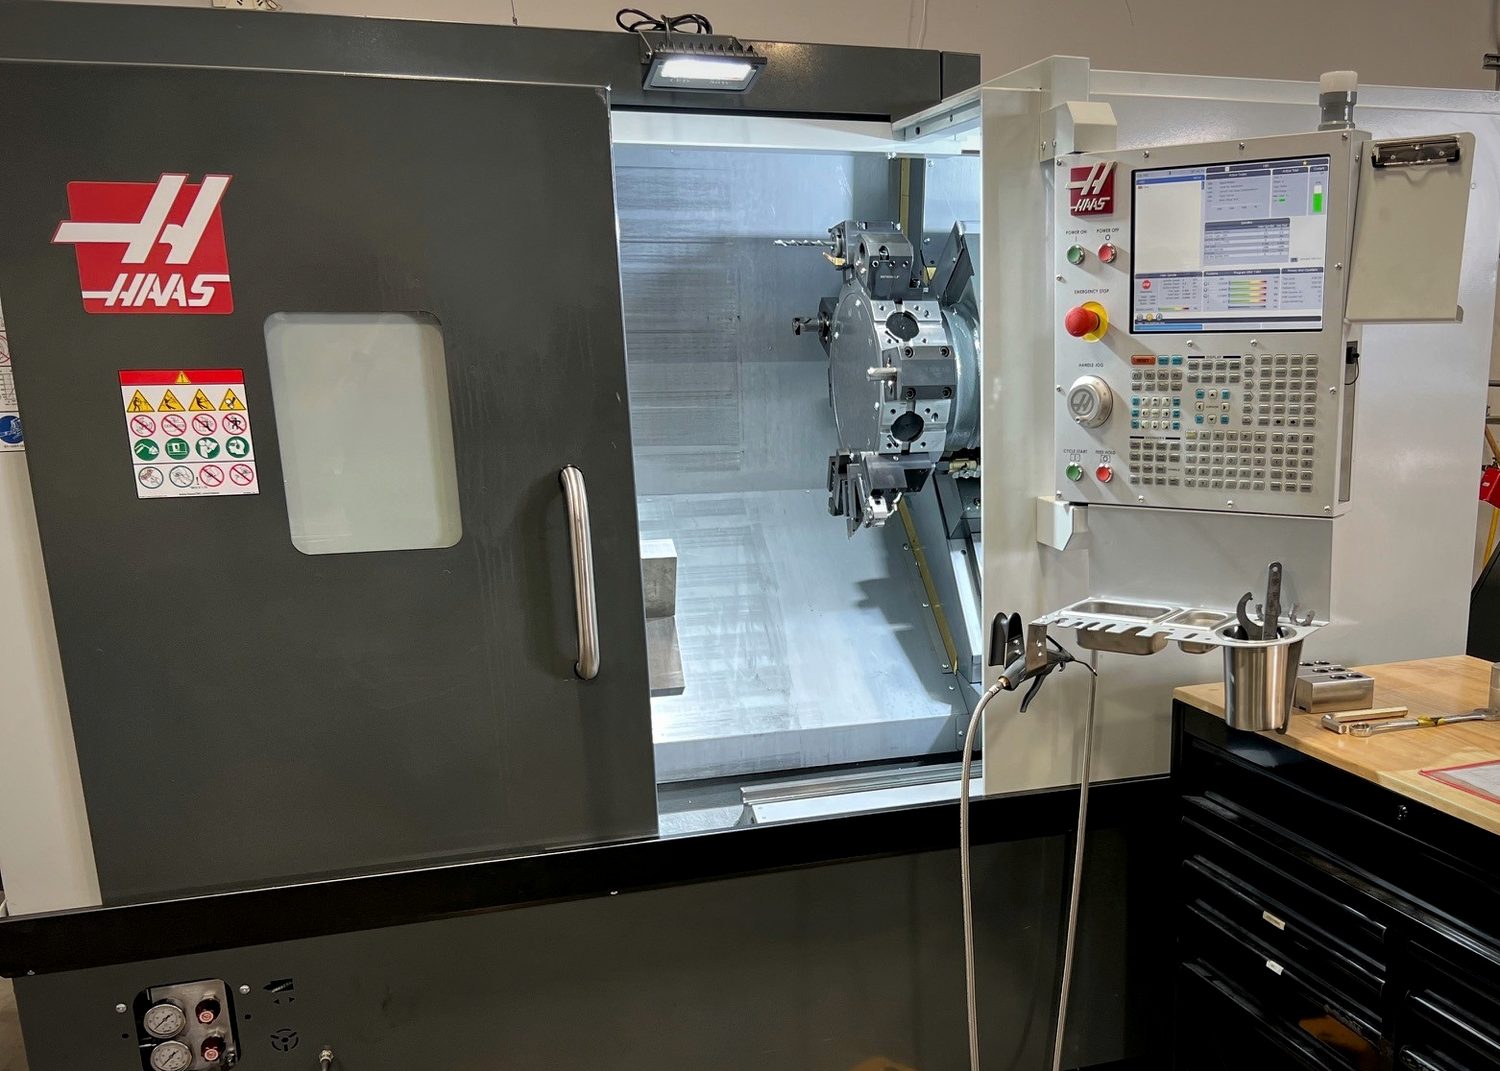
Turning centers with live tooling and sub-spindle capability complete the front and back of a part in one handling. Fewer setups mean tighter concentricity, better repeatability, and less opportunity for error on complex turned components.
- Long, slender, and thin-walled turned parts
- Cross-holes, flats, and milled features in the same setup
- Precision threads, bores, and sealing surfaces
02 Milling
Precision milling
Multi-axis milling for prismatic components, housings, fixtures, and detail work where flatness, position, and surface finish are called out and inspected. Programmed, fixtured, and proven in-house before production begins.
- Tight-tolerance pockets, bores, and datum structures
- Complex contours and compound angles
- Fixture design and workholding built here
03 Automation
Robotic machine tending
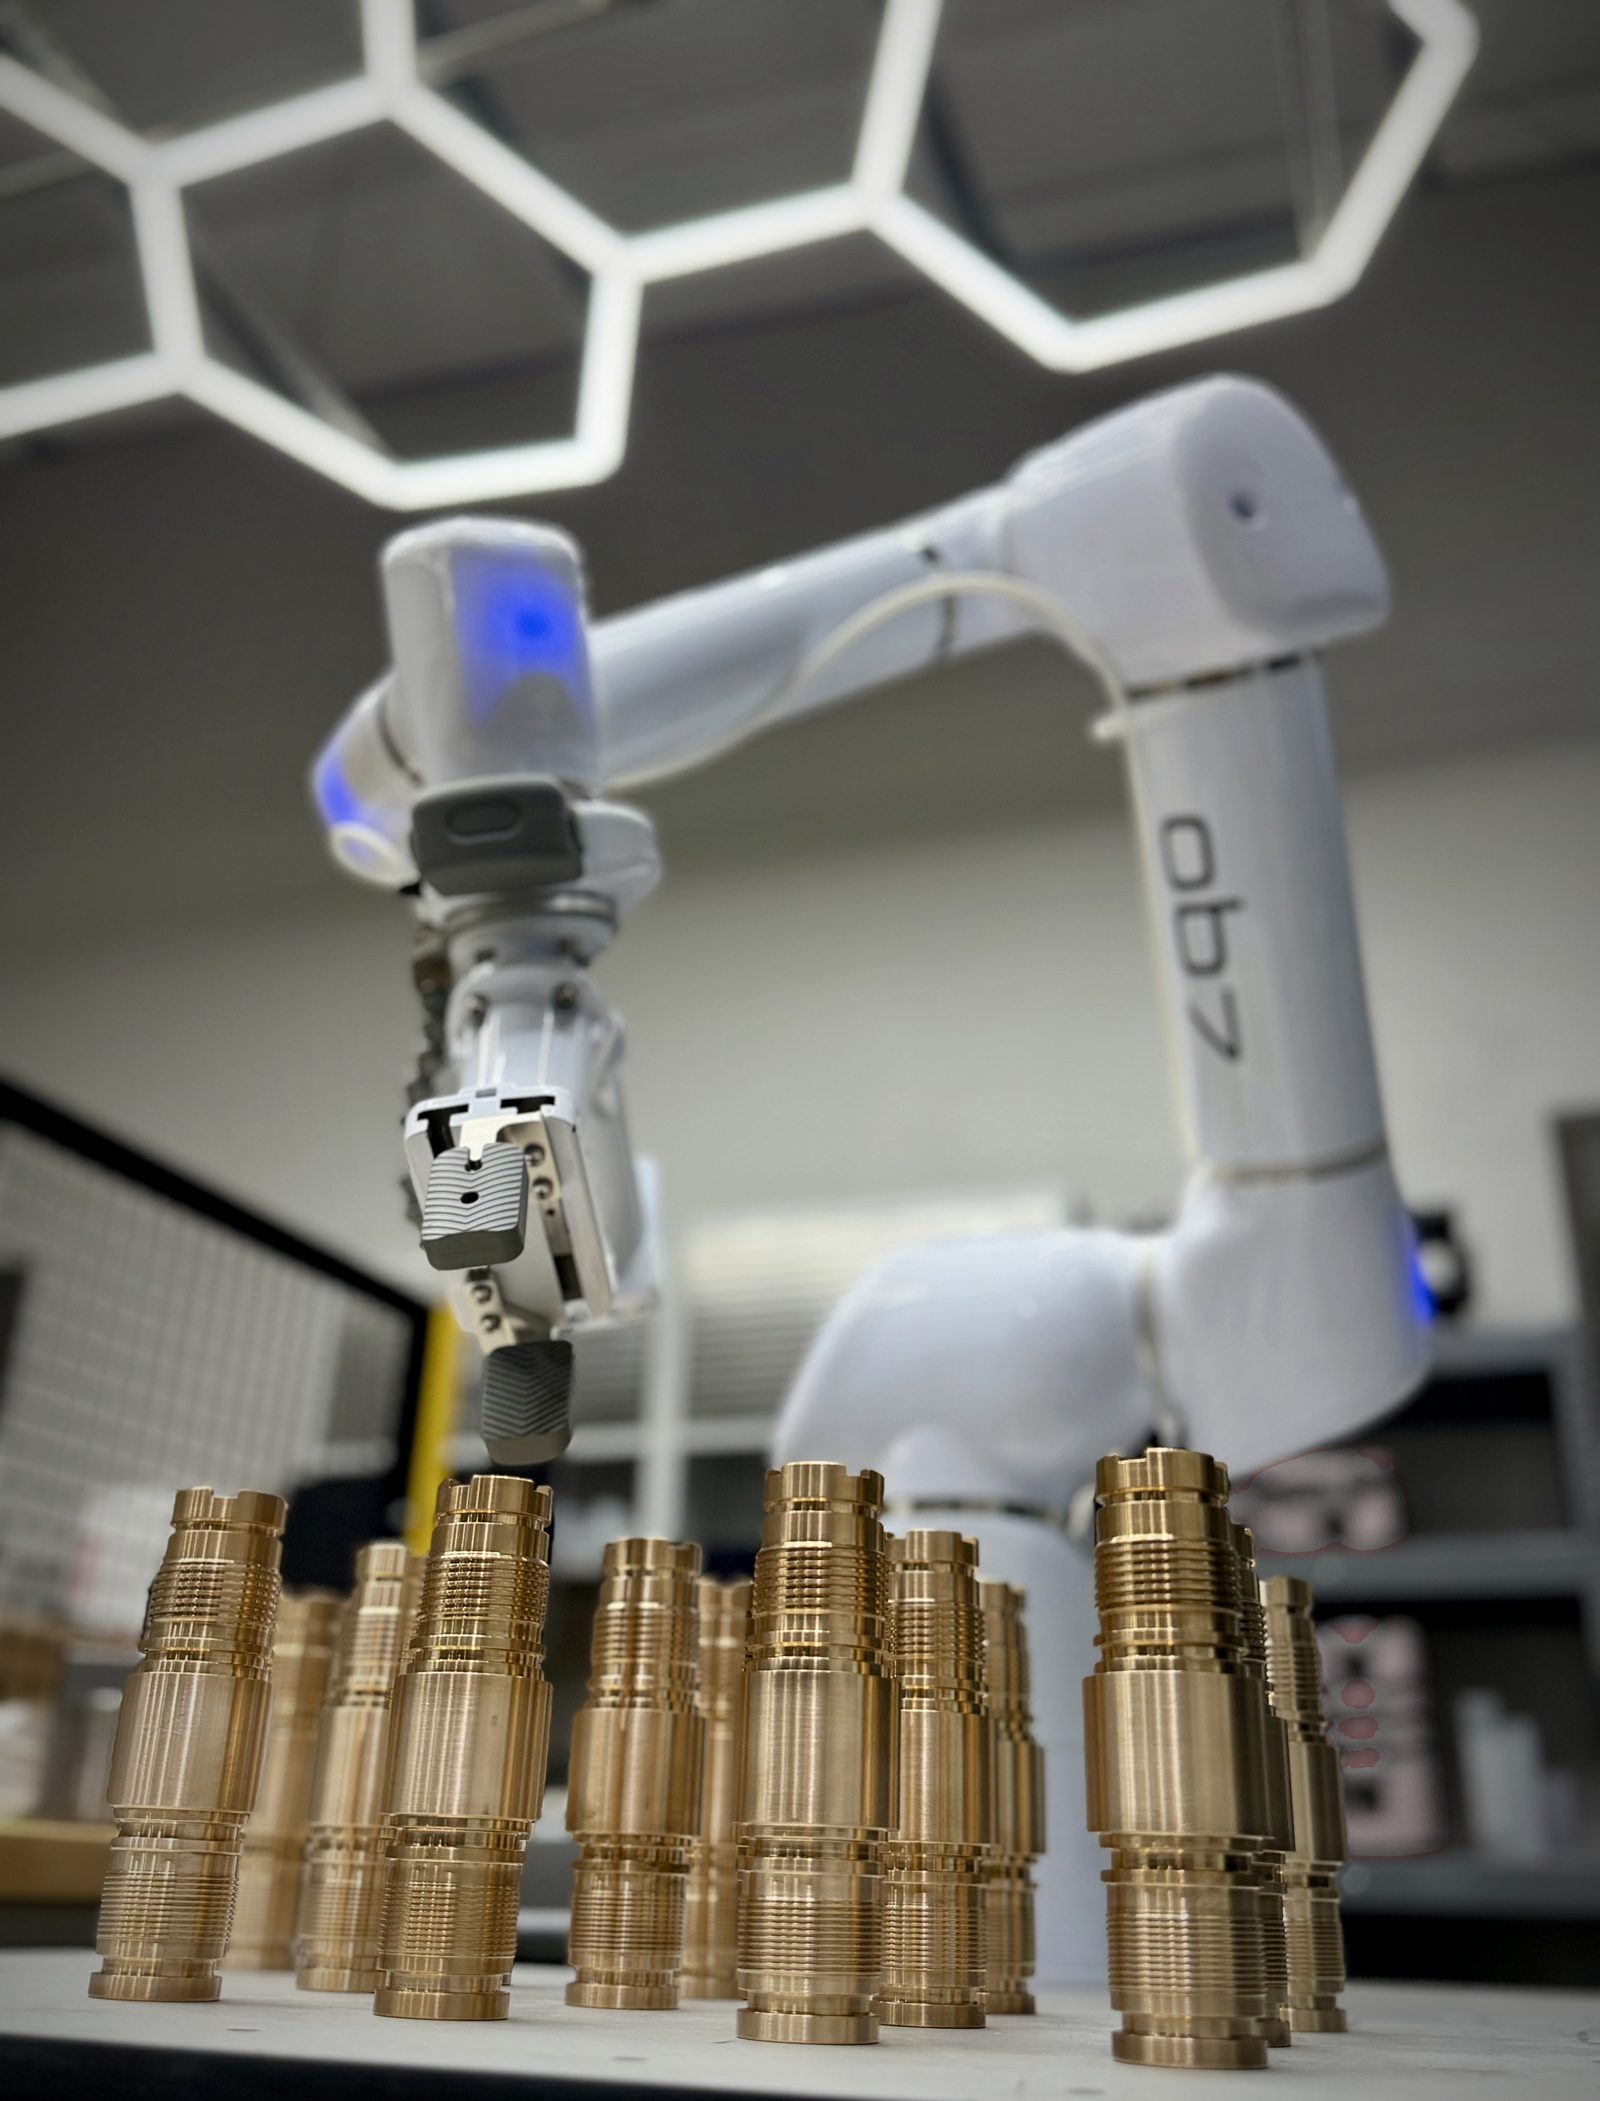
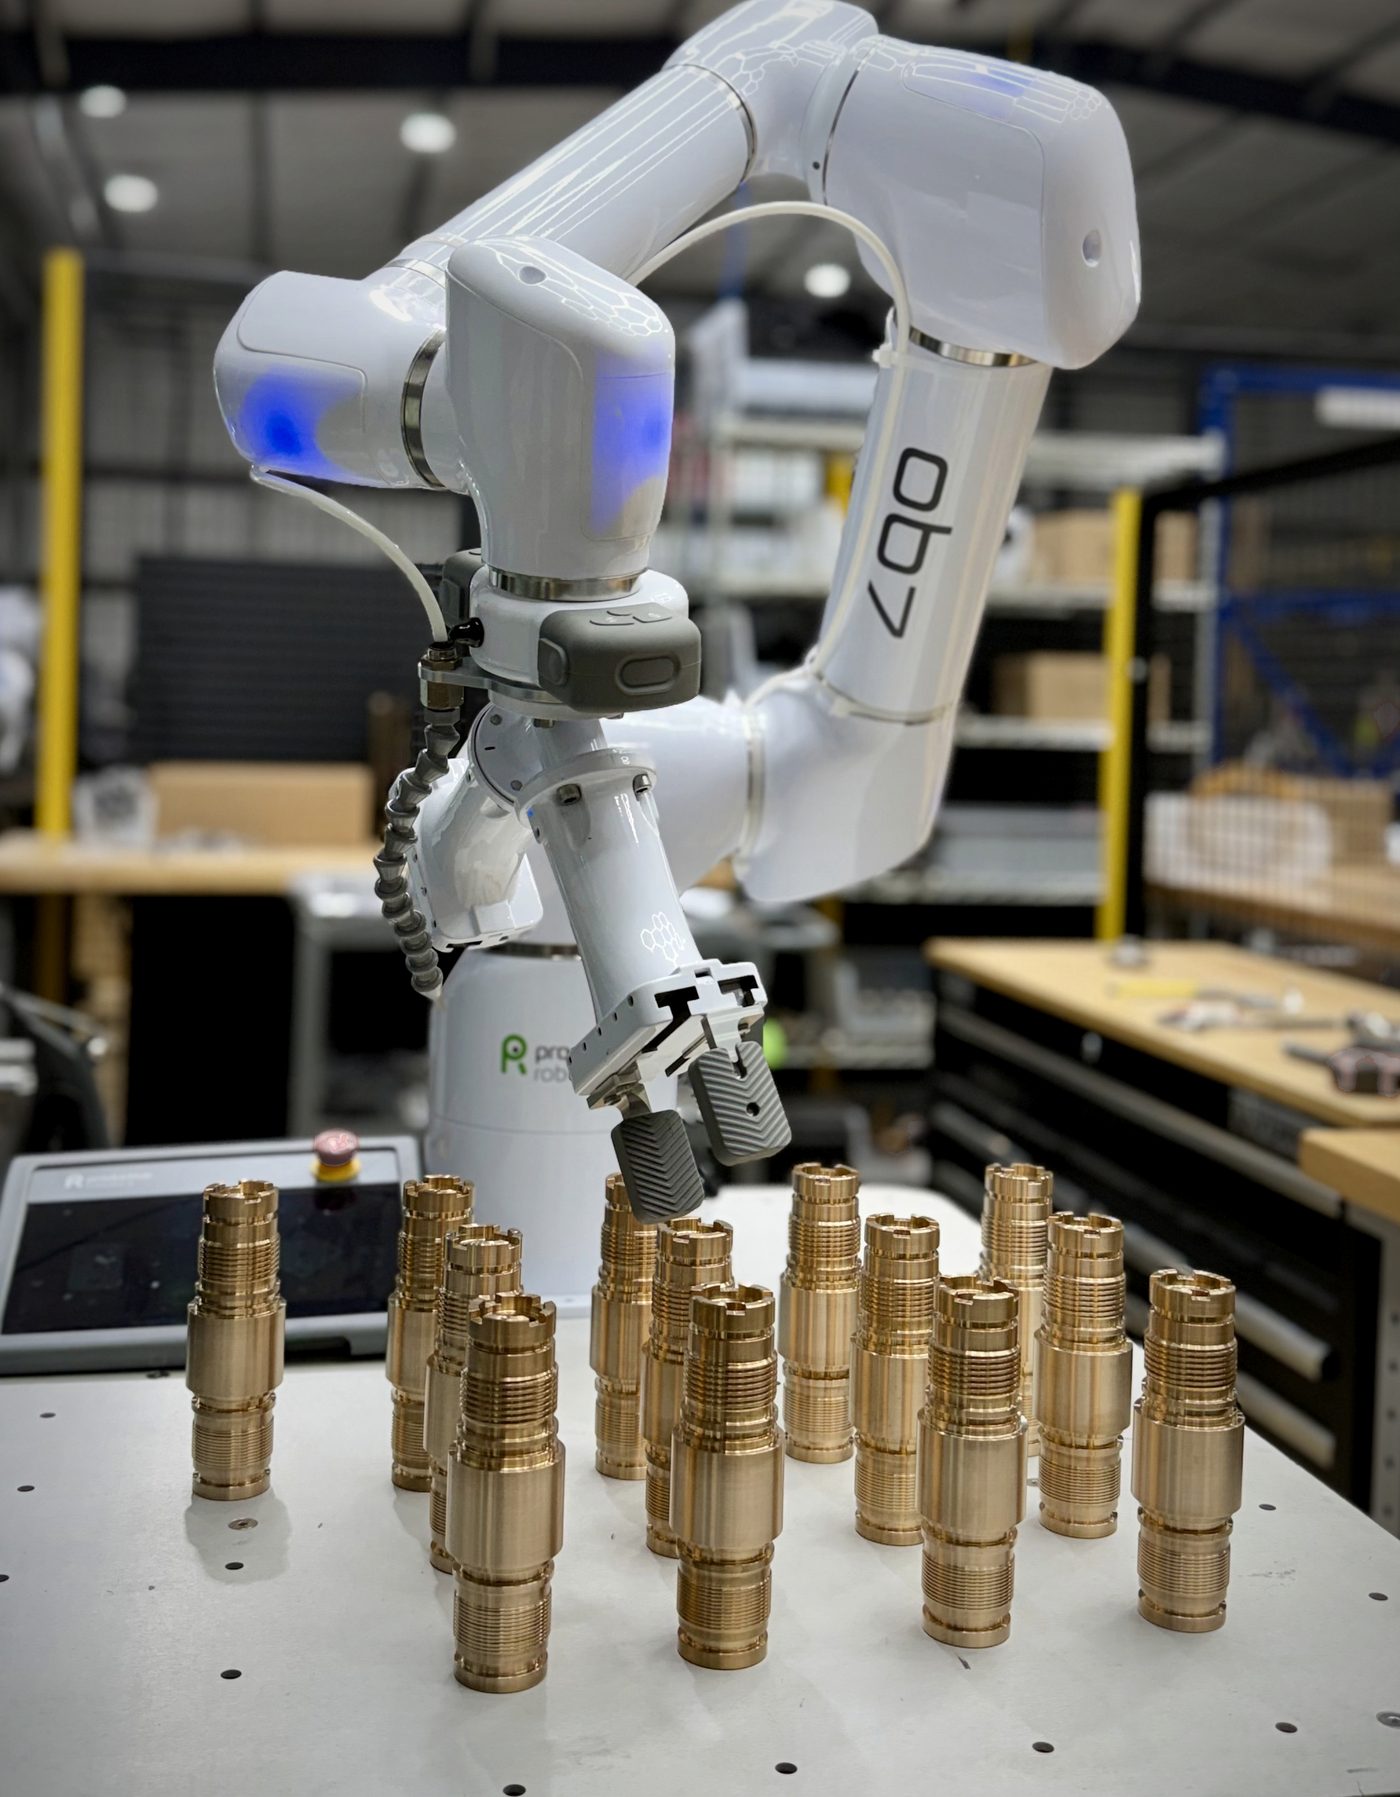
Collaborative robots load, unload, and stage parts so spindles keep cutting through unattended hours. For repeat production, that translates into consistent cycle-to-cycle quality, predictable capacity, and delivery dates we can commit to.
- Lights-out and extended-shift production
- Stable pricing on established part numbers
- Capacity that scales with your release schedule
04 Materials
Difficult materials, done routinely
Work-hardening stainless, gummy copper alloys, and tough nickel alloys behave differently at the cutting edge. We select tooling, speeds, coolant, and workholding for the material, not for the catalog, and we hold that recipe once it is proven.
- Non-magnetic and austenitic stainless steels
- Beryllium copper and other high-strength copper alloys
- Nickel-based alloys, alloy and tool steels, aluminum
05 Engineering
Process engineering
Every job starts with a print review and a manufacturing plan: tooling, workholding, sequence, inspection points, and secondary operations. Programming and prove-out happen on our floor, so first articles arrive with a process behind them, not a guess.
- Design-for-manufacturability feedback before you commit
- Documented first-article inspection
- Locked process for repeat releases
06 Finishing
Finished, not just machined
Heat treat, plating, coatings, marking, and assembly are managed through vendors we have qualified and hold accountable. You issue one purchase order and receive one finished, inspected, certified part, with the paperwork to match.
- Secondary operations coordinated and inspected on return
- Certifications and traceability assembled in one package
- See the full list of managed services below
Materials we run
A representative list, not a limit. If your print calls for something else, send it. We will tell you plainly whether it is a fit.
Beryllium copperToughMetNitronic & non-magnetic stainless300 & 400 series stainless17-4 PHInconel & nickel alloys4140 & 4340Tool steelsAluminumBrass & bronzeEngineering plastics
Material certifications are retained by heat and lot and travel with the part. Customer-supplied material is welcome and tracked the same way.